Originally published: September 30, 2011
Last updated: October 19, 2026
At a time when most power plants are worried about meeting new EPA regulations, one Colorado coal-fired power plant that boasts about being among the top ten lowest emitters in the nation due to modern dust collection systems (or colector tipo baghouse) looks to improve even more; it claims other plants give coal a bad name.
How Did Rawhide Energy Station Become a Leader in Low-Emission Coal Power Generation?
Baghouse.com – September 31st, 2011, Fort Collins, Colorado – Rawhide Energy Station, located 26 miles north of Fort Collins, CO, is held in high esteem as an example of what a 21st-century coal-fired power plant should be. The plant that is owned by four local municipalities through the Platte River Power Authority (PRPA), currently ranks in the top ten in the country for lowest emissions despite being a 280-megawatt facility.
What has enabled Rawhide Energy Station to stand out among its fellow coal-fired plants by maintaining such high environmental standards, while still proving to be a profitable enterprise? Plant staff believe it’s the dedication they take to environmental responsibility that is echoed throughout the entire operation.
“The whole coal industry gets a bad name when there’s a big difference between a facility like this and a facility that doesn’t even spray or have a baghouse,” stated plant manager Jason Frisbie. “These are existing technologies that would make all these plants much cleaner than they are right now. Proven.” The plant staff counts a history of always investing in new technologies to attain even lower emissions than required by current regulations.
Rawhide Energy Station's Extensive Pollution Control Systems
Rawhide Energy Station currently averages SO2 emissions of .081 pounds per million BTUs (British Thermal Units), about one tenth of the average of .765 PPM. The plant currently operates several pollution control systems concurrently to handle the various pollutants generated by the coal combustion process. The most extensive of these is the boiler itself, which is a Combustion Engineering (now Alstom Power) tangentially fired (T-fired) boiler equipped with a new low-NOx burner system in fall of 2005. For additional NOx collection, the plant operates a dry spray absorber. For SO2 collection, the plant uses a Joy Niro dry scrubber system and an activated carbon injection system for mercury (Hg) control. Two baghouses with approximately 6,500 PTFE membrane 34-foot filter bags are used to achieve particulate matter (PM2.5) collection efficiencies. The colector tipo baghouse collectors also assist in the collection of excess dry scrubbing product from the scrubbers, and are integral in the operation of the activated carbon injection system used for mercury (Hg) collection.
The plant uses a lot of coal – about 1.25 million tons a year -brought in by rail from Wyoming. They also maintain a 60-day reserve in case supply is ever interrupted. The main type of coal used to operate the plant’s main boiler is Powder River Basin (PRB) coal, a sub-bituminous type of coal that is mined from large deposits in Wyoming and Montana. This type of coal, while producing fewer BTUs per ton than other types, is highly valued due to its substantially low sulfur content, which aids in keeping SO2 emissions low.
However, there is a trade-off with using low-sulfur coal. Sub-bituminous coal leads to increased difficulty in collecting mercury emissions, which have recently become regulated by the EPA (Environmental Protection Agency). The PRPA has taken steps to reach compliance with these new regulations even before they come into effect by installing an activated carbon injection system for mercury control. The system works by injecting activated carbon, which absorbs the hard-to-collect elemental forms of mercury (Whereas bituminous coal creates mainly oxidized forms that are easier to collect). The mercury-laden carbon is then collected in the colector tipo baghouse on the surface of the ePTFE (Teflon) membrane filter bags, which in turn when cleaned, allows for the collection and disposal of the mercury along with other collected particles such as fly ash. This technology represents the newest environmental focus of the industry with the new EPA regulations coming into effect in the near future. However, as we can see, the Rawhide Energy Station already prepared well in advance for the coming regulations, in line with the plant’s self-motivated philosophy of striving to operate more environmentally friendly.
With all of this APC (air pollution control) technology, surely the plant must suffer from extensive downtime for system installation and additional maintenance. However, is that the case?
"We Focus on Preventive...and Predictive Maintenance"
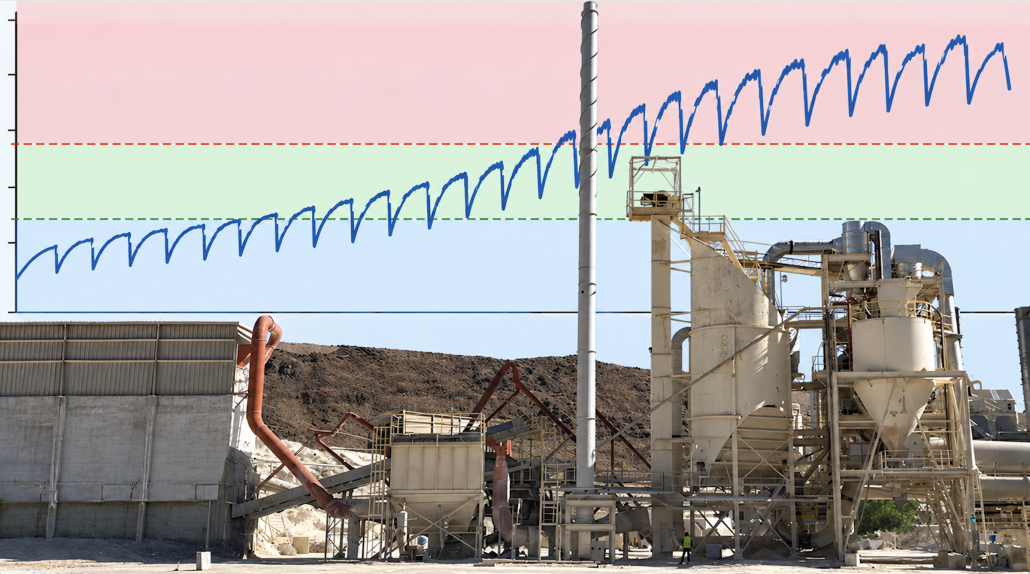
By placing a high value on preventive maintenance, the plant has been able to achieve a relatively high average capacity factor (how much the plant puts out compared to its full potential). The plant currently has a lifetime equivalent availability factor of around 98% with its capacity factor about 88.8%. “A lot of plants manage about 70 percent,” says Doug Adair, maintenance manager for the plant. This has not come about without a lot of forethought and planning. The plant usually plans for a full-scale shutdown every three to five years. This enables the plant to prevent small problems (such as replacing filters in the bag house) from becoming larger ones (damage to plant systems from higher emissions due to lower bag house performance).
In addition to the main coal-fired boiler, the plant also fields four GE Frame 7EA natural gas-fired turbines totaling 260 MW (three installed in 2002 and a fourth added in 2004). These are used to provide additional power during peak hours.
“We focus a lot on preventive maintenance and predictive maintenance”
– Doug Adair Maintenance Manager
Company Mindset Contributes to Stellar Record
It all starts with the people and a teamwork culture that shares ownership of the facility. Jason Frisbie, the division manager of Power Production at Rawhide, noted that “while the operating statistics and utilization of technology continue to pay off, the primary reason for Rawhide’s success can be attributed directly to the dedicated and professional staff at the station.”Here is an example of Rawhide’s unique management culture. Each employee, including the plant manager, is assigned a cleaning area that requires that person’s attention for an hour a week. Individuals feel a sense of accomplishment when they’re done, and everyone has a facility that all are proud of. Another benefit of a good, clean, safe work environment is that it’s easier to spot problems with the equipment and easier to fix those problems as well.
Despite seeing demand drop substantially from its peak two years ago, during which time the plant ran all its gas turbine units in addition to the coal-fired unit, the plant continues to provide plenty of work for over one hundred full-time employees.
The peak position may be the control room — no one gets in there until they’ve had at least 15 years’ experience. Many have 25, almost as long as the plant’s been up and running.”So Homer Simpson couldn’t work here,” City Councilwoman Sarah Levison joked during a recent plant tour. You are correct,” Adair said. “Homer Simpson couldn’t work here.”
“Homer Simpson couldn’t work here.”
– Maintenance Manager Doug Adair commenting on the level of experience required of the plant’s operators
Unique Environmental View Leads to Unconventional Success
Following the pattern of the unique environmental philosophy, the plant, in addition to its extensive pollution control equipment, also takes a more symbolic approach to build its environmentally friendly image. In the early days of the area now known as Fort Collins, thousands of wild Bison roamed this area and called it home. According to Albert Hamilton, Platte River Power Authority’s first general manager, “Bison should be returned to the grasslands to symbolize the ruggedness of the American West and to demonstrate that power plants can coexist in harmony with native plants and wildlife.”
The plant established a program called “Adopt-a-Buffalo” in 1983 to bring back some of that sense of oneness with nature to the plant. From the first twenty bison, the herd has produced numerous award-winning animals. Profits from sales offset the cost of the program. Plant staff help take care of the herd, providing water and feed for the herd.
The program’s success is satisfying proof for plant management that their efforts to protect the environment are working. “Any corporation, any company, doesn’t have to destroy what’s around them to be successful,” says spokeswoman Rae Todd.
More About the Rawhide Energy Station:
In 1973, the cities of Longmont, Fort Collins, Loveland and Estes Park joined to create Platte River Power Authority. The PRPA operates the Rawhide Energy Station north of Fort Collins and provides power for all the previously mentioned municipalities. Each municipality sets the rates for its own jurisdiction.
Director of Operations | Dust Collection Specialist | Industrial Filtration Consultant
Dominick DalSanto is an author and environmental technologies expert specializing in dust collection systems. He has nearly a decade of hands-on working experience in the industry. Dominick is the sales director and sales technical advisor for an industrial dust collection equipment manufacturer. Personally took the lead on key projects each year from sales engineer to field advisor to project manager to business relations. Born in San Bernardino County, California, and raised in Chicago, he currently resides in Buenos Aires, Argentina.